
An allergen statement tells you what is in the drum. It says nothing about what was in the equipment four hours earlier. For a phosphatidylserine purchase programme, that distinction is the whole risk. PS is a small-volume, high-value ingredient, and the plants that make it rarely run it alone — the same blenders, dryers, sieves and packing lines handle carriers, excipients, spray-dried flavours and botanical extracts, some of which carry milk, wheat, egg, peanut or tree nut proteins.
The realistic hazard is therefore not the composition of the PS itself but carryover from the previous campaign. That is controlled by three things: how the schedule is sequenced, how the line is cleaned between products, and how cleaning is verified before the next batch is released. None of those three appears in a one-page declaration, and none is answered by asking a supplier whether it is "allergen free".
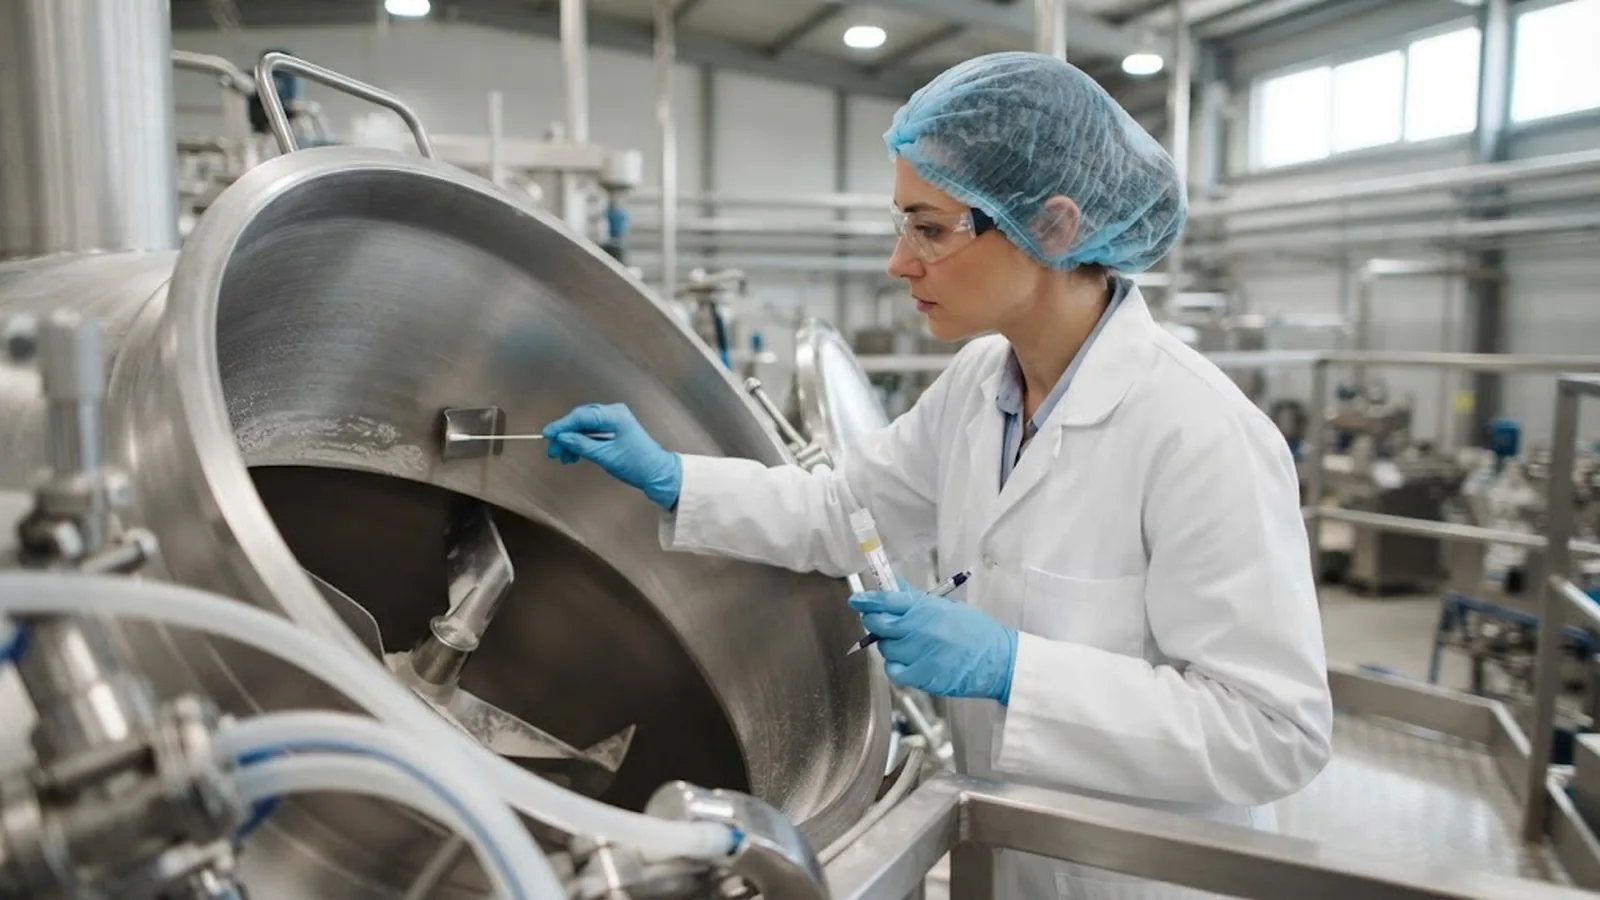
!QA analyst swabbing stainless steel processing equipment for allergen residue during a cleaning validation in a powder ingredient plant Where source selection is part of the decision, our soy phosphatidylserine page documents the extraction, specification and paperwork behind the soy route.
Why an Allergen Statement Is Not Cross-Contact Evidence
Both regulatory systems push allergen control into the supplier's food safety system rather than into a single document. In the US, the major food allergens are defined by the Food Allergen Labeling and Consumer Protection Act and extended by the FASTER Act, and facilities are expected to treat allergen cross-contact as a hazard under the preventive-controls rules in 21 CFR Part 117. In the EU, Regulation (EU) No 1169/2011, Annex II, fixes the list of substances that must be declared, with narrow exemptions for certain highly refined derivatives.
Neither regime hands you a numeric cross-contact threshold to rely on. EU risk assessment for precautionary labelling works from published reference doses and action levels; US law sets no general threshold below which a precautionary statement becomes unnecessary. The declaration you receive is a legal summary of composition and, at best, a conclusion about the plant. When your finished-product label says "may contain milk", that liability sits with your brand, which is why the changeover and cleaning records belong in the approval file rather than in a request you make after a customer complaint.
Map the Changeover Matrix Around Your PS Campaign
The first document to request is a changeover matrix: which products run on the PS line, in what standard order, which of them carry declared allergens, what cleaning is applied after each, and whether a minimum run separation applies before a PS campaign.
Two details separate a real matrix from a decorative one. Sequencing: if the plant schedules allergen-bearing products before allergen-free ones, cleaning carries more of the load and the validation evidence must be stronger. And wet versus dry changeovers: a line cleaned by vacuum and wipe behaves differently from one that receives a wet clean and a full dry-out, and equipment that cannot be wet-cleaned — a fluid-bed dryer, a classifier, certain mills — usually cannot reach the same cleanliness by dry methods alone. If your supplier's line is dry-clean only and the preceding campaigns are allergen-bearing, that is the conversation to have, not the declaration.
What a Cleaning Validation Report Must Contain
A cleaning validation report is verifiable when it contains five elements. Missing any one of them, you are reading a narrative rather than evidence.
- A parameterised procedure: the exact sequence of steps, the detergent or solvent and its concentration, contact or circulation time, temperature and the mechanical action. "Cleaned thoroughly" is not a procedure.
- Acceptance criteria set in advance, with the derivation shown — a health-based limit derived from a reference dose, or a defined limit per square centimetre of product-contact surface.
- A sampling plan naming worst-case locations, not the easiest ones: corners, gaskets, dead legs, the underside of dryer trays, sieve inlets and chute transitions.
- Recovery data for the sampling method. A swab result without a known recovery percentage is not a quantitative result.
- Repeat runs with a stated conclusion. A single successful run demonstrates that cleaning happened once; it does not validate a procedure.
If no such file exists for the equipment that will make your PS, ask whether the plant relies on visual cleanliness alone — defensible for some non-allergen changeovers, not for allergen ones.
Sampling and Method: Swab, Rinse, ELISA and PCR
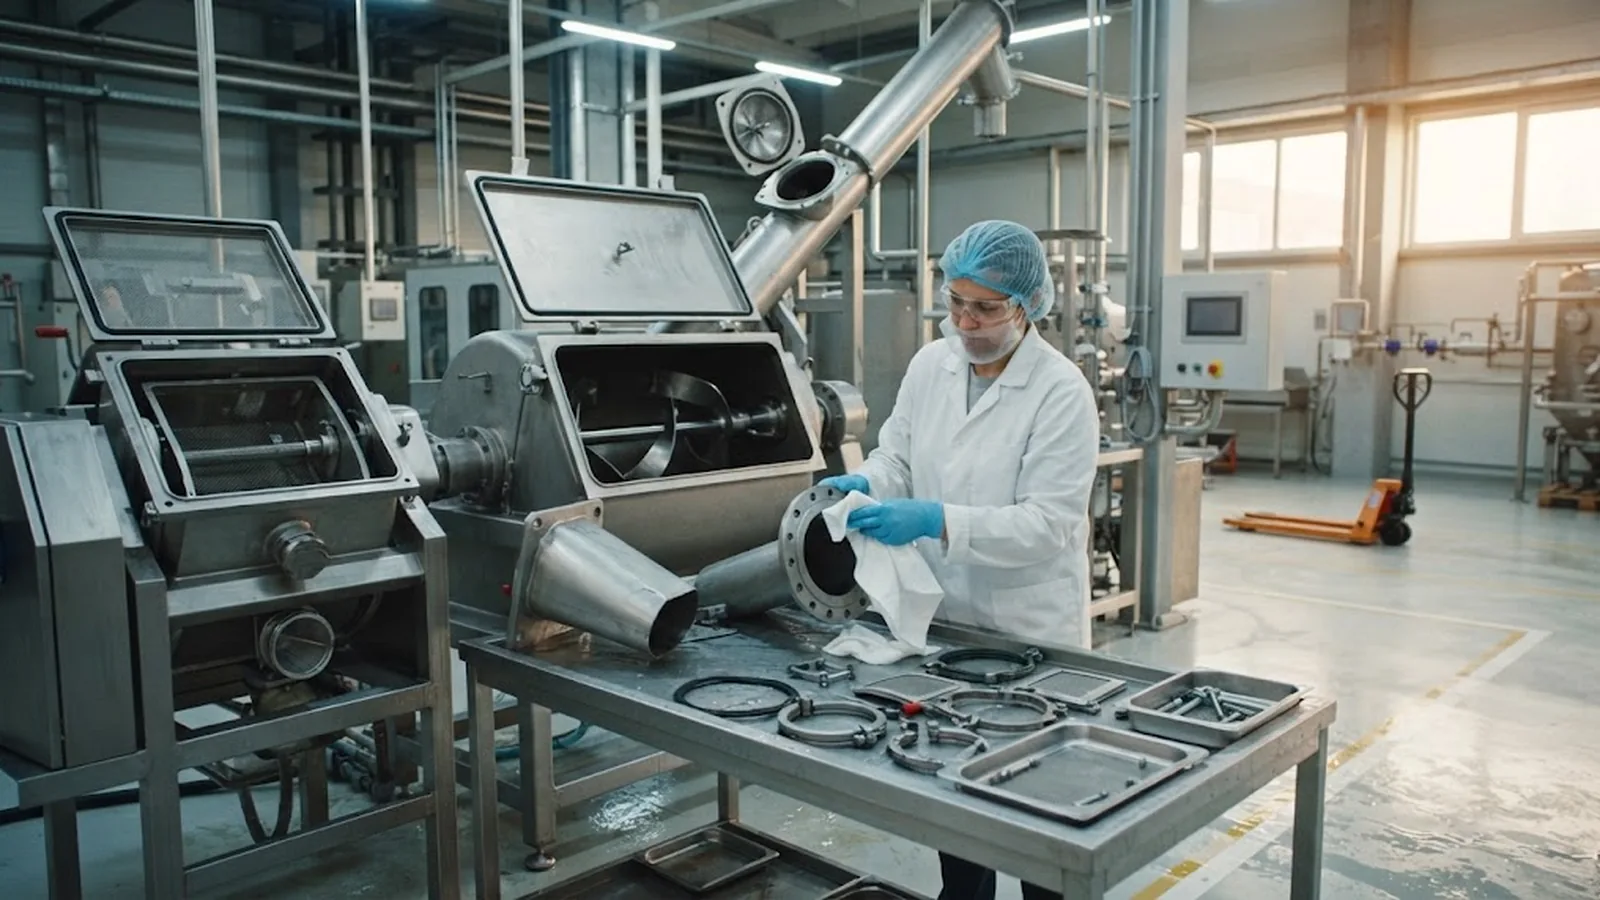
Swabbing product-contact surfaces is the standard approach on dry equipment, because it targets where carryover actually transfers. Rinse sampling suits closed systems that can be filled and drained. Agree the reporting unit before accepting any number: nanograms per square centimetre is comparable between sites, whereas parts per million in a rinse volume is not unless the surface area and rinse volume are stated. Sampling after dry-down better represents the state of the line when the next product is charged.
On method choice, ELISA detects the allergenic protein and is the closer proxy for consumer risk. PCR detects DNA, which often survives processing but says nothing about whether allergenic protein survived — a negative PCR is reassuring but is not proof of protein absence. Rapid lateral-flow devices are useful for routine qualitative checks and do not replace quantitative validation. Three biases belong in your interpretation rules: kit target differences, matrix effects from phospholipid residue, and incomplete swabbing that produces a low result resembling good cleaning. When a positive screen appears, follow a decision tree rather than rejecting the lot: confirm with a second method, re-sample, and evaluate against the action level. Zero is not achievable on a shared line, and specifying it creates disputes you cannot win.
Verification Frequency and the Quality-Agreement Clauses
Initial validation shows the procedure works when performed correctly. Routine verification shows it keeps working. Re-verify at trigger events: a new allergen-bearing product on the line, a change in cleaning chemistry or sequence, maintenance on product-contact equipment, a long shutdown, or a new operator cohort. Between triggers, the normal monitoring is visual inspection plus periodic verification on a defined cadence. Cost matters: every swab carries a laboratory price, and a supplier asked to test every changeover will price it into your material. Set the trigger list explicitly and review the cadence at the annual supplier review.
Four clauses make the controls survive staff turnover. Change notification before a new allergen-bearing product enters the line or a cleaning procedure changes, with updated validation data attached. The right to take retention samples for independent testing, with an agreed retest protocol. A named documentation list, so the changeover matrix, procedure and validation summary are controlled documents supplied with the technical file. And a failure protocol: who investigates an exceeded action level, how affected lots are held and how the root cause is closed out. A supplier that can demonstrate all four gives you the option of a simpler precautionary statement on pack — which is a commercial advantage on a supplement shelf.
FAQ
Q: Is phosphatidylserine itself an allergen?
A: Phosphatidylserine is a phospholipid and is not a listed food allergen in either the US or the EU. If the PS is soybean-derived, the soy origin may still trigger a declaration depending on processing and the exemptions that apply, so confirm the position for your exact ingredient and market with your regulatory function.
Q: What is the difference between an allergen statement and a cross-contact control file?
A: The statement describes the composition of the material. The control file documents the plant: which allergen-bearing products share the equipment, how the line is cleaned between them, the validated acceptance criteria and the verification results. Only the second tells you anything about carryover risk.
Q: Can a supplier claim "allergen free" for PS made on a shared line?
A: On a genuinely shared multi-product line, a categorical claim is difficult to defend regardless of cleaning performance. The defensible position is a validated changeover procedure with verification data and, where the risk assessment supports it, a precautionary statement naming the specific allergens that could carry over.
Q: Should allergen carryover be tested with ELISA or PCR?
A: ELISA for the allergenic protein is the better default for validating a cleaning procedure, because it measures the hazard that matters. PCR is a useful cross-check where processing has degraded the protein, but its result must be read alongside the protein data, not instead of it.
Q: How often should allergen verification testing be repeated?
A: After initial validation, re-verify at trigger events — a new allergen-bearing product on the line, a change in cleaning chemistry or sequence, maintenance on product-contact equipment, a shutdown or an operator change — plus a periodic confirmation during steady operation.
Conclusion
Allergen control for a phosphatidylserine purchase programme is a documentation and plant-verification exercise, not a labelling exercise. The declaration you receive should be the cover page of a file containing a changeover matrix, a parameterised cleaning procedure, acceptance criteria with a derivation, a sampling plan with recovery data and repeat-run results — plus a verification cadence and a failure protocol. Buyers who ask for that file at supplier qualification, rather than after a positive screen, end up with a defensible label and a supplier relationship grounded in data. When you are ready to move from checklist to quotation, contact our team with the grade, source and document set described above.
Sources
- U.S. Food and Drug Administration — Food Allergen Labeling and Consumer Protection Act (FALCPA) and allergen guidance: https://www.fda.gov/food/food-allergensgluten-free-guidance-documents-regulatory-information
- U.S. Electronic Code of Federal Regulations — 21 CFR Part 117, Current Good Manufacturing Practice, Hazard Analysis, and Risk-Based Preventive Controls for Human Food: https://www.ecfr.gov/current/title-21/chapter-I/subchapter-B/part-117
- European Union — Regulation (EU) No 1169/2011 on the provision of food information to consumers (Annex II): https://eur-lex.europa.eu/eli/reg/2011/1169/oj
- FAO / WHO Codex Alimentarius — Code of Practice on the Management of Food Allergens for Food Business Operators: https://www.fao.org/fao-who-codexalimentarius/codex-texts/codes-of-practice/en
- ISO — ISO 22000 food safety management systems: https://www.iso.org/iso-22000-food-safety-management.html
Buyer fit
Who this guide is for
This guide is written for the buyer profiles below. Open your profile for the matching grades, documents and next steps, or tell us your requirements directly.
Recommended next steps
- Review the Phosphatidylserine product page.
- Compare Soy PS and Sunflower PS.
- Check manufacturing proof and Quality & R&D.
Contact sales for product documents
Share source preference, application, country, and annual quantity.
Contact Sales